
In modern industrial operations, efficiently moving liquids laden with solid particles is a critical challenge. Submersible slurry pumps have become the go-to equipment across numerous sectors, offering unparalleled performance, adaptability, and reliability. Whether in mining, wastewater management, or chemical processing, these powerful tools streamline operations, reduce costs, and enhance productivity.
1.What Is a Submersible Slurry Pump and How Does It Work
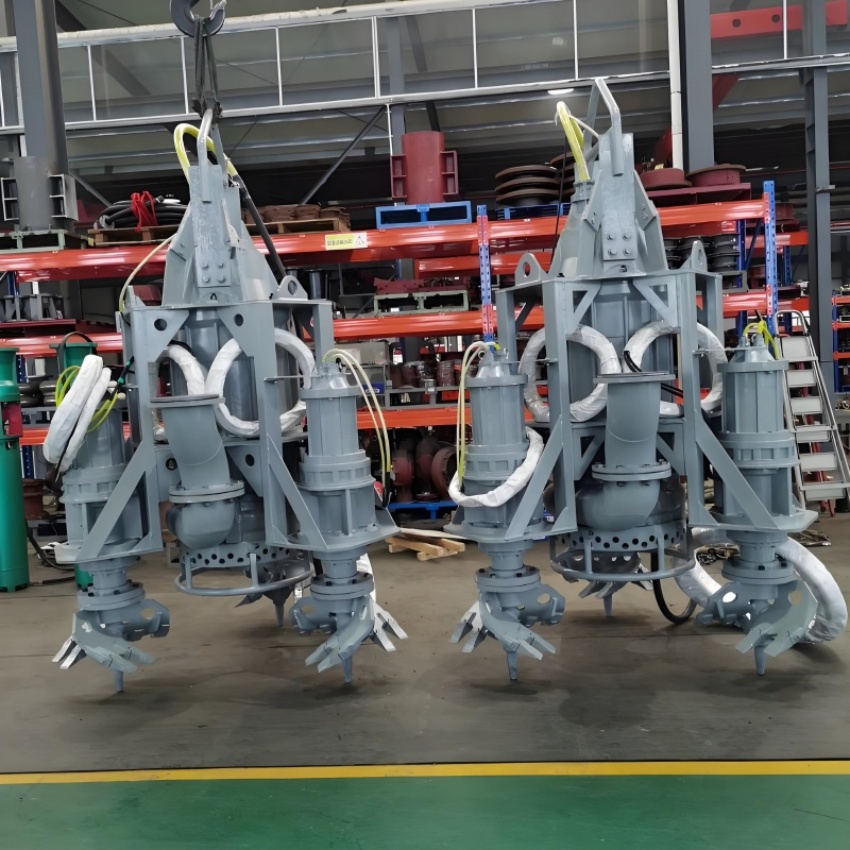
A submersible slurry pump is an integrated unit designed to operate while fully submerged in the fluid it is pumping. Unlike traditional pumps, it combines a sealed motor and pump assembly into a single robust structure. When activated, the motor drives the impeller, transferring kinetic energy to the slurry. This process suspends solid particles within the liquid and propels them through the discharge line.
Key advantages of this design include
No need for priming
Elimination of auxiliary installation components
Reduced space requirements
Ability to handle high solid concentrations
This makes these pumps ideal for challenging and dynamic environments, from deep mining operations to temporary construction sites.


2.Key Industries Benefiting from Submersible Slurry Pumps
2.1. Mining and Mineral Processing
Submersible slurry pumps are critical in transporting ore slurries, tailings, and processing by-products. They are used extensively in gold, copper, and iron ore mines to move abrasive mixtures from extraction points to processing plants. Their ability to operate underwater and in confined spaces increases both safety and efficiency.
2.2. Power Generation
In coal-fired power plants, these pumps handle ash slurry, remove slag, and assist in hydraulic conveying systems. They are also used in coal preparation plants for moving coal-water mixtures and supporting flue gas desulfurization processes.
2.3. Metallurgical Operations
From transporting molten slag to handling grinding circuits in smelters, these pumps endure extreme temperatures and abrasive conditions. Special materials like high-chrome alloys or ceramic linings are often used to extend service life.
2.4. Construction and Tunneling
Submersible slurry pumps dewater excavation sites, pump mud from foundations, and manage seepage in tunnels. Their portability and quick setup make them invaluable for keeping construction sites dry and safe.
2.5. Environmental and Wastewater Management
These pumps are used in
Dredging rivers and lakes
Pumping sludge in treatment plants
Handling leachate in landfills
Managing stormwater and sewage
Their clog-resistant design ensures continuous operation even with fibrous and solid waste materials.
2.6. Chemical and Industrial Processing
Capable of handling corrosive and abrasive fluids such as acidic slurries or crystalline suspensions these pumps are constructed with materials like stainless steel, rubber, or polyurethane to resist chemical attack.
2.7. Oil and Gas Sector
In drilling operations, submersible slurry pumps move drilling mud, assist in well cleanup, and help in sand and solids handling during extraction and recovery processes.
2.8. Water Infrastructure Management
Used in irrigation, dam maintenance, and canal dredging, these pumps ensure water systems remain free of silt and debris, supporting agricultural and public water supply networks.
2.9. Pulp and Paper Industry
They transport high-density pulp, recycle process water, and manage waste from paper production, contributing to both efficiency and sustainability.
3.Why Choose a Submersible Slurry Pump
Energy Efficiency
Advanced hydraulic designs reduce power consumption while delivering high flow rates and heads, resulting in significant operational savings.
Exceptional Durability
Constructed with wear-resistant materials, these pumps withstand harsh conditions, minimize downtime, and lower long-term maintenance costs.
Easy Installation and Mobility
Their submersible nature eliminates the need for fixed foundations or suction piping. They can be deployed quickly and moved easily between sites.
Reliability in Demanding Conditions
With superior sealing and cooling capabilities often using the fluid itself for cooling, these pumps offer continuous operation without overheating or failure.
Broad Compatibility
From slurries and sewage to chemically aggressive fluids, these pumps handle a wide range of viscosities, temperatures, and pH levels.
Low Maintenance Needs
Modular designs and accessible components simplify inspection, cleaning, and part replacement further reducing lifecycle costs.

4.What Users Are Saying
Mining Project Manager, Malaysia
We switched to submersible slurry pumps last year and saw a 30 percent increase in processing capacity. Downtime has dropped dramatically, and the pumps handle abrasive slurries better than any previous equipment.
Water Treatment Engineer, Chile
These pumps manage high-solid sludge without clogging. We have reduced maintenance frequency and costs, and improved overall system reliability.
Site Supervisor, Maldives
On our coastal construction project, submersible pumps handle saline water and sand effortlessly. Quick to deploy and extremely dependable.
Process Engineer, China Chemical Plant
We transport highly corrosive crystalline slurries with these pumps. Their material integrity and performance under extreme conditions are impressive.
The Future of Submersible Slurry Pumps
As industries push for greater efficiency and sustainability, submersible slurry pumps continue to evolve. Innovations in smart monitoring, improved materials, and energy-saving designs are expanding their applications. Companies that adopt these advanced pumps benefit from reduced operational costs, enhanced environmental compliance, and increased productivity.
5.Conclusion
Submersible slurry pumps are indispensable in today’s industrial landscape. Their versatility, durability, and efficiency make them the preferred choice for handling the most demanding solid-liquid mixtures across a wide range of sectors. Investing in the right slurry pump not only improves operational performance but also offers significant economic and environmental advantages.
Whether you are in mining, water treatment, construction, or manufacturing, there is a submersible slurry pump designed to meet your needs ensuring that your operations run smoother, longer, and more cost-effectively.
Keywords submersible slurry pump, solid-liquid handling, mining pumps, wastewater sludge pump, abrasive slurry pump, industrial pumping solutions, dredging pump, construction dewatering, chemical slurry pump, high-efficiency slurry pump.
Authored by
Alina.Liu
Email: Oceanpump15@tsbeng.com
WhatsApp: +86 17354610320


